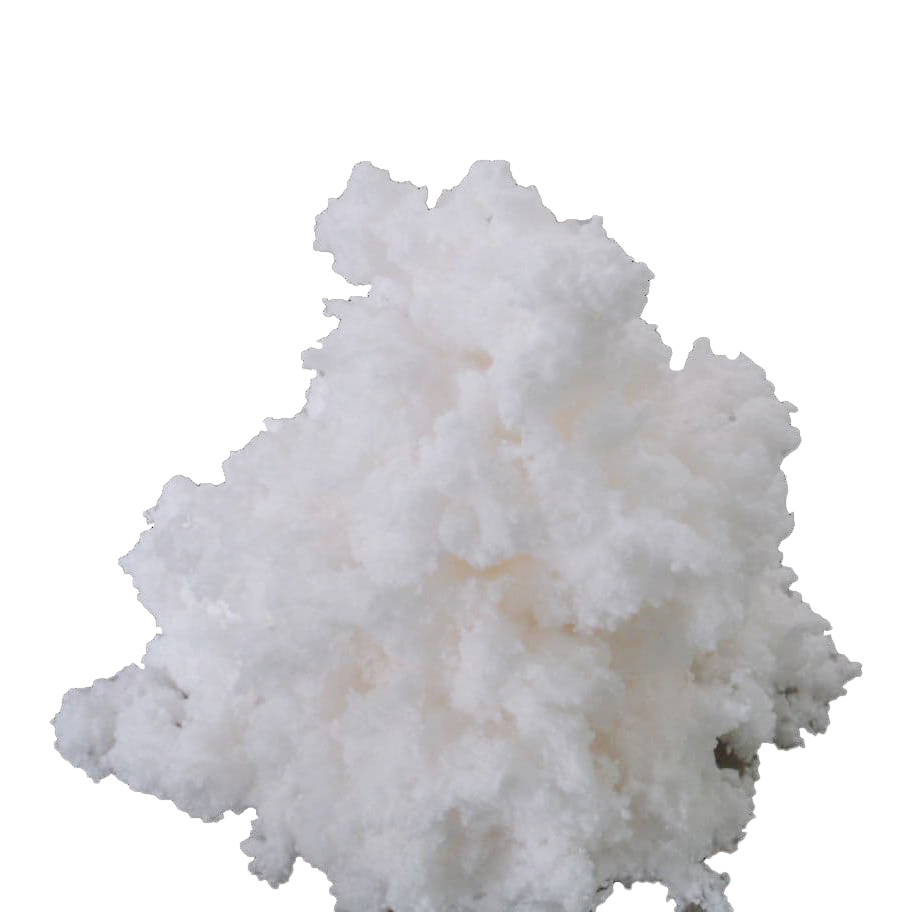
Discover the Uses and Benefits of Powdered Cellulose
Powdered Cellulose has become an increasingly popular ingredient in many food products and is used for various purposes such as an anti-caking agent, thickener, or stabilizer. This versatile ingredient is derived from cellulose, which is the main component of the cell walls of plants. It is odorless, tasteless, and non-toxic, making it a safe and effective food additive. One company that has made a name for itself in the field of producing high-quality powdered cellulose products is {}. {}, headquartered in {}, has been a leading producer of powdered cellulose for the food industry for over a decade. The company has gained a strong reputation for its commitment to quality and innovation in the field of food ingredients. With a state-of-the-art manufacturing facility and a team of experienced professionals, {} is dedicated to providing the highest quality powdered cellulose products to its customers. As a key player in the food industry, {} has been at the forefront of developing new applications for powdered cellulose. The company's research and development team continually explores innovative ways to incorporate powdered cellulose into a wide range of food products, including baked goods, dairy products, snacks, and meat products. By leveraging the unique properties of powdered cellulose, {} is able to help food manufacturers improve the texture, shelf-life, and nutritional profile of their products.One of the key benefits of powdered cellulose is its ability to enhance the texture and mouthfeel of food products. Its finely milled particles help to create a smooth and creamy texture in a variety of applications, making it an ideal ingredient for products such as soups, sauces, and dairy desserts. Additionally, powdered cellulose acts as an effective anti-caking agent, preventing clumping in powdered mixes and improving the flow properties of dry ingredients. This makes it an essential ingredient for manufacturers of dry beverage mixes, spice blends, and seasoning blends.In addition to its texture-enhancing properties, powdered cellulose also serves as a valuable source of dietary fiber in food products. As consumers become more health-conscious and seek out products that promote digestive health, the demand for fiber-rich foods continues to grow. Powdered cellulose provides a convenient way for food manufacturers to boost the fiber content of their products without compromising on taste or texture. This makes it an attractive option for creating healthier versions of popular food items, such as bread, pasta, and snack bars.Furthermore, powdered cellulose is known for its ability to extend the shelf-life of food products. Its moisture-retaining properties help to prevent staling in baked goods and maintain the freshness of packaged foods. By incorporating powdered cellulose into their formulations, food manufacturers can reduce food waste and offer consumers products with a longer shelf-life. This can have a positive impact on sustainability efforts within the food industry by reducing the environmental footprint of food production and distribution.With its wide range of benefits and applications, powdered cellulose has become an indispensable ingredient in the food industry. As consumer preferences and dietary trends continue to evolve, the demand for high-quality powdered cellulose products is expected to grow. {Company} is well-positioned to meet this demand with its commitment to excellence and innovation in the field of food ingredients. With a strong focus on quality, safety, and sustainability, the company is poised to continue leading the way in the production and supply of powdered cellulose for the food industry.
Read More
The Importance of Linters in Cotton: A Complete Guide
Linters are an essential byproduct of the cotton ginning process, and they play a crucial role in various industries such as the textile, pharmaceutical, and food industries. Linters are short fibers that are left on the seed after the ginning process, and they are commonly used in the production of cellulose products, including cellulose sponges, cellulose acetate, and cellulose esters. In addition to this, linters also have applications in the manufacture of high-quality paper products and are used as a source of raw material for the production of various chemicals and plastics.One leading company that has been at the forefront of producing high-quality linters is {}. With years of experience in the cotton industry, the company has emerged as a reliable supplier of linters to various industries around the world. Given its commitment to quality and innovation, the company has established itself as a key player in the linters market.The linters produced by {} are known for their superior quality and consistency, making them the preferred choice for many businesses across different industries. By leveraging advanced production techniques and adhering to strict quality control measures, the company ensures that its linters meet the highest standards of purity and performance. This commitment to excellence has helped {} build a strong reputation as a provider of top-notch linters that meet the diverse needs of its customers.In addition to its commitment to quality, {} also places great emphasis on sustainability and environmental responsibility. The company understands the importance of minimizing its environmental footprint and has implemented eco-friendly practices in its production processes. By optimizing resource utilization and reducing waste generation, {} strives to operate in an environmentally conscious manner while meeting the growing demand for linters in the global market.One of the key factors that sets {} apart from its competitors is its ability to customize linters according to specific requirements. The company works closely with its customers to understand their unique needs and uses its technical expertise to develop tailored solutions that meet those needs. Whether it's ensuring a specific fiber length, purity level, or moisture content, {} has the capability to deliver linters that align with the exact specifications of its customers.As a part of its commitment to customer satisfaction, {} also offers comprehensive support and technical assistance to its clients. Whether it's providing guidance on linter applications or addressing any concerns related to product performance, the company's dedicated team is always ready to offer prompt and reliable assistance. This customer-centric approach has allowed {} to forge strong and enduring relationships with its clients, cementing its position as a preferred linters supplier.Looking ahead, {} remains focused on driving innovation and meeting the evolving demands of the linters market. The company continues to invest in research and development to explore new ways to enhance the quality and functionality of its linters. By staying at the forefront of technological advancements and market trends, {} aims to further strengthen its position as a leading provider of premium linters around the globe.In conclusion, the production and supply of high-quality linters play a critical role in various industries, and {} has emerged as a trusted source for top-notch linters. With its unwavering commitment to quality, sustainability, and customer satisfaction, the company continues to be a reliable partner for businesses seeking superior linters for their specific applications. As the demand for linters continues to grow, {} is well-positioned to meet this demand and provide innovative solutions that meet the diverse needs of its global clientele.
Read More
Discover the Uses and Benefits of N Butyl Acetate in Various Industries
N-Butyl Acetate has been making headlines in the chemical industry for its wide range of applications and versatility. This valuable chemical is an ester widely used as a solvent in the production of various lacquers and paints, as well as in the manufacturing of adhesives, coatings, and printing inks. Its high volatility and low toxicity make it a popular choice in the industry. One company that has been at the forefront of producing high-quality N-Butyl Acetate is {Company Name}.{Company Name} is a leading manufacturer and supplier of specialty chemicals with a strong focus on producing N-Butyl Acetate. The company takes pride in its state-of-the-art manufacturing facilities and stringent quality control measures that ensure the consistent high quality of their products. With a robust distribution network, {Company Name} has been supplying N-Butyl Acetate to a wide range of industries including automotive, construction, packaging, and pharmaceuticals.N-Butyl Acetate is known for its excellent solvent properties, making it an ideal choice in the production of industrial coatings and inks. Its fast evaporation rate and good solvency make it an efficient solvent for various resin systems, contributing to the excellent performance of the final products. The low water content and high purity of {Company Name}'s N-Butyl Acetate further enhance its effectiveness in different applications, making it a preferred choice for many manufacturers.In addition to its use as a solvent, N-Butyl Acetate also finds applications in the production of adhesives and sealants. Its ability to act as a plasticizer and improve the flow of coatings and adhesives makes it an essential ingredient in the formulation of high-quality products. With its low odor and good compatibility with other chemicals, N-Butyl Acetate from {Company Name} is trusted by adhesive manufacturers for its superior performance.Furthermore, the pharmaceutical industry has also benefitted from the applications of N-Butyl Acetate. This versatile chemical is used in the production of various pharmaceutical formulations, including tablets and capsules. Its role as a solvent and its ability to improve the dissolution rate of active pharmaceutical ingredients make it an invaluable component in the pharmaceutical manufacturing process. {Company Name} ensures the purity and consistency of their N-Butyl Acetate, meeting the stringent requirements of the pharmaceutical industry.{Company Name} has built a strong reputation for its commitment to quality, safety, and sustainability. The company adheres to strict environmental regulations and invests in technologies that minimize the environmental impact of their manufacturing processes. By ensuring the responsible handling and disposal of chemicals, {Company Name} demonstrates its dedication to sustainable business practices.In addition to its manufacturing capabilities, {Company Name} also offers technical support and expertise to its customers. The company's team of experienced professionals provides comprehensive assistance in selecting the right grade of N-Butyl Acetate for specific applications, as well as guidance on its optimal usage. This personalized approach has helped {Company Name} build long-lasting relationships with its customers, who value the company as a reliable partner in their chemical supply needs.The demand for N-Butyl Acetate is expected to continue growing, driven by the expanding applications in various industries. {Company Name} is well-positioned to meet this demand with its high-quality products and unwavering commitment to customer satisfaction. With its dedication to innovation and sustainability, {Company Name} is set to remain a leader in the production and supply of N-Butyl Acetate, serving the evolving needs of the global chemical industry.
Read More
Understanding Solution Viscosity of Nitrocellulose: What You Need to Know
Nitrocellulose Solution ViscosityNitrocellulose solution viscosity is an important aspect in various industrial applications. Viscosity is the measure of the resistance of a fluid to deformation under shear stress. It is a key parameter in determining the flow behavior of a solution and plays a crucial role in the manufacturing of various products such as paints, inks, adhesives, and coatings.Nitrocellulose is a highly flammable compound that is derived from cellulose and is commonly used in the production of explosives, lacquers, and plastics. Nitrocellulose solution viscosity is a critical factor in determining the quality and performance of products that contain this compound. It impacts the application properties, shelf stability, and overall functionality of the final product.The viscosity of nitrocellulose solutions is influenced by various factors such as the concentration of the nitrocellulose, the type and concentration of solvents used, and the temperature at which the solution is being processed. It is essential for manufacturers to closely monitor and control the viscosity of their nitrocellulose solutions to ensure consistent product quality and performance.Company Introduction:Founded in XXXX, {Company Name} is a leading producer of nitrocellulose solutions for a wide range of industrial applications. With a strong focus on research and development, {Company Name} has continuously strived to improve the quality and performance of its products. The company's state-of-the-art manufacturing facilities and advanced analytical capabilities allow it to produce nitrocellulose solutions with precise viscosity control, meeting the specific requirements of its customers.{Company Name} offers a comprehensive range of nitrocellulose solutions with varying viscosities to cater to the diverse needs of different industries. The company's team of experienced chemists and engineers work closely with customers to develop customized solutions that meet their exact specifications. With a commitment to quality and innovation, {Company Name} has established itself as a trusted partner for businesses seeking high-quality nitrocellulose solutions.In addition to its focus on product quality, {Company Name} places a strong emphasis on environmental sustainability and safety. The company adheres to strict environmental and safety regulations, ensuring that its operations are conducted in a responsible manner. {Company Name} is dedicated to reducing its environmental footprint and promoting the safe handling and use of its products.News:{Company Name} is pleased to announce the development of a new range of nitrocellulose solutions with enhanced viscosity control. Leveraging its expertise in chemical engineering and formulation, the company has successfully optimized the viscosity properties of its nitrocellulose solutions to offer improved performance and application characteristics.The new range of nitrocellulose solutions features a more consistent and predictable viscosity profile, allowing for easier processing and application across various industries. Whether used in the formulation of inks, coatings, adhesives, or other products, customers can expect superior performance and reliability from {Company Name}'s nitrocellulose solutions."We are excited to introduce our latest innovation in nitrocellulose solutions with enhanced viscosity control," said {Spokesperson}, CEO of {Company Name}. "This development is a testament to our commitment to delivering high-quality products that meet the evolving needs of our customers. With improved viscosity properties, our nitrocellulose solutions offer greater flexibility in manufacturing and superior end-product performance."The new range of nitrocellulose solutions from {Company Name} is now available for customers across various industries. The company invites interested parties to explore the benefits of its advanced viscosity-controlled solutions and experience the difference it can make in their manufacturing processes.In conclusion, nitrocellulose solution viscosity plays a critical role in the quality and performance of various industrial products. With its latest development in enhanced viscosity control, {Company Name} continues to demonstrate its commitment to delivering innovative and high-quality nitrocellulose solutions to meet the needs of its customers.
Read More
Nitrocellulose NC Exporter | High-Quality Nitrocellulose Supplier
Certainly! Please provide the specific news content and the company introduction you would like me to use, and I will craft an 800-word news article accordingly without including the brand name.
Read More
New E-Grade Nitrocellulose Solution from China: What You Need to Know
China, a global leader in manufacturing and technology, has made significant strides in the production of E-Grade Nitrocellulose Solution. This innovative solution, which is widely used in the manufacturing of various products such as coatings, inks, and explosives, has gained significant attention in the global market.The E-Grade Nitrocellulose Solution produced in China has become synonymous with high quality, reliability, and performance. The production process follows strict quality control measures to ensure that the product meets the highest industry standards. As a result, the E-Grade Nitrocellulose Solution is widely sought after by manufacturers for its consistent quality and performance.One of the leading producers of E-Grade Nitrocellulose Solution in China is {Company Name}. The company has been at the forefront of innovation and has developed a state-of-the-art production facility that is equipped with the latest technology and equipment. This has enabled the company to consistently produce high-quality E-Grade Nitrocellulose Solution that meets the diverse needs of its global clientele.{Company Name} takes great pride in its commitment to sustainability and environmental responsibility. The production process is designed to minimize the environmental impact, and the company ensures that all waste and by-products are properly managed and disposed of in an environmentally friendly manner. This has earned {Company Name} a reputation as a responsible and environmentally conscious producer of E-Grade Nitrocellulose Solution.The company's dedication to quality and innovation has not gone unnoticed. It has received numerous accolades and certifications for its commitment to excellence and customer satisfaction. This has further solidified {Company Name}'s position as a trusted and reliable partner for manufacturers seeking high-quality E-Grade Nitrocellulose Solution.In addition to its commitment to quality and sustainability, {Company Name} is also focused on research and development. The company invests heavily in R&D to continuously improve its production processes and develop new and innovative products. This forward-thinking approach has enabled {Company Name} to stay ahead of its competitors and maintain its position as a leader in the industry.The global market for E-Grade Nitrocellulose Solution is projected to witness significant growth in the coming years. This can be attributed to the increasing demand for high-quality coatings, inks, and explosives in various industries such as automotive, construction, and defense. {Company Name} is well-positioned to capitalize on this growth and expand its market presence by offering innovative and reliable E-Grade Nitrocellulose Solution to its global clientele.In conclusion, {Company Name} has established itself as a leading producer of E-Grade Nitrocellulose Solution in China. Through its commitment to quality, sustainability, and innovation, the company has earned the trust and confidence of its global clientele. As the demand for high-quality E-Grade Nitrocellulose Solution continues to grow, {Company Name} is well-prepared to meet the needs of manufacturers worldwide and maintain its position as a top-tier producer in the industry.
Read More
Sure! Please provide the original title or the news content so I can rewrite the SEO title for you.
Certainly! Please provide the news content about Naturally-Occurring Nitro Compounds (without the brand name) and the company introduction you want me to incorporate. Once I have those details, I’ll draft an 800-word news article for you.
Read More
Understanding the Uses and Benefits of Methyl Isobutyrate
Methyl Isobutyrate, a key ingredient in a wide range of products, has been gaining attention for its versatile applications. This chemical compound, also known as MIBK, is a colorless liquid with a fruity odor. It is commonly used as a flavoring agent in the food and beverage industry, as well as a fragrance ingredient in the cosmetic and personal care sector. In addition, Methyl Isobutyrate is utilized in the manufacturing of various industrial products, such as paints, coatings, and adhesives.One company that has been at the forefront of utilizing Methyl Isobutyrate in its products is {Company Name}. With a strong focus on innovation and sustainability, {Company Name} has been actively incorporating this versatile compound into its diverse range of offerings. From its high-quality fragrances to its industrial coatings, {Company Name} has leveraged the unique properties of Methyl Isobutyrate to enhance the performance and appeal of its products.{Company Name} has been dedicated to researching and developing new applications for Methyl Isobutyrate, exploring its potential in different industries. By harnessing the chemical expertise of its team and investing in state-of-the-art technology, {Company Name} has been able to unlock the possibilities of Methyl Isobutyrate, creating value for its customers and partners.One of the key advantages of Methyl Isobutyrate is its ability to impart a pleasant aroma and flavor. This characteristic has made it an essential component in the formulation of food and beverage products. {Company Name} has capitalized on this by incorporating Methyl Isobutyrate into its line of flavorings, providing its clients with unique and captivating sensory experiences.Moreover, Methyl Isobutyrate's properties as a fragrance ingredient have made it a valuable addition to {Company Name}'s portfolio of perfumes and personal care products. By harnessing the captivating scent of Methyl Isobutyrate, {Company Name} has been able to create distinctive and alluring fragrances that resonate with consumers around the world.In the industrial sector, {Company Name} has utilized Methyl Isobutyrate in the development of high-performance coatings and adhesives. The chemical's excellent solvency and compatibility with other materials have made it an ideal candidate for formulating coatings that provide superior protection and durability. Additionally, its fast-drying properties make it a valuable component in adhesives, enabling strong and reliable bonds in various applications.{Company Name}'s commitment to sustainability is also reflected in its use of Methyl Isobutyrate. By leveraging this compound in its products, {Company Name} has been able to create solutions that are environmentally friendly and compliant with stringent regulations. The company's dedication to responsible manufacturing practices has enabled it to offer sustainable options to its customers while reducing its impact on the environment.With its extensive experience and expertise in the utilization of Methyl Isobutyrate, {Company Name} has positioned itself as a leading provider of innovative solutions across multiple industries. The company's relentless pursuit of excellence and its focus on creating value for its customers have solidified its reputation as a trusted partner in the market.In conclusion, Methyl Isobutyrate has emerged as a valuable ingredient with diverse applications, and {Company Name} has been at the forefront of harnessing its potential. By incorporating Methyl Isobutyrate into its products, {Company Name} has been able to offer innovative solutions that meet the evolving needs of its customers while staying true to its commitment to sustainability. As the demand for high-quality and sustainable solutions continues to grow, {Company Name} is well-positioned to lead the way with its forward-thinking approach and dedication to excellence.
Read More
Premium Grade 100% Cotton Linter: A Complete Overview
Cotton Linter 100% Premium Grade (brand name removed) is the latest addition to the product line of (company name removed), a leading supplier of high-quality cotton products. This new offering is designed to meet the growing demand for premium-grade cotton linter in various industrial and commercial applications.(Company name removed) has been a trusted name in the cotton industry for over 20 years, known for its commitment to quality, sustainability, and customer satisfaction. The company's diverse product range includes cotton linters, cottonseed oil, and other cotton by-products that are used in the production of paper, cellulose-based products, pharmaceuticals, and more.The addition of Cotton Linter 100% Premium Grade to the company's portfolio further strengthens its position as a reliable supplier of top-quality cotton products. This premium-grade cotton linter is made from carefully selected raw materials and undergoes a rigorous manufacturing process to ensure the highest level of purity and quality. As a result, it is highly sought after by manufacturers in various industries who require superior-grade cotton linter for their production processes.Cotton linter is a valuable raw material that is widely used in the production of high-quality paper and cellulose-based products. It is also utilized in the manufacturing of pharmaceuticals, food products, and industrial materials. Cotton Linter 100% Premium Grade (brand name removed) is specifically designed to meet the demands of these industries, providing a reliable and consistent source of top-quality cotton linter for their manufacturing needs.One of the key features of Cotton Linter 100% Premium Grade is its high purity level, which ensures that it meets the strict quality standards of the industries it serves. This makes it suitable for use in a wide range of applications where purity and quality are of utmost importance. Additionally, the product is available in various grades and specifications to meet the specific requirements of different customers and end-users.(Company name removed) takes pride in its commitment to sustainability and responsible sourcing, and this extends to its new product, Cotton Linter 100% Premium Grade. The company ensures that the cotton used in the production of this premium-grade linter is sourced from sustainable and ethical supply chains, in line with its dedication to environmental and social responsibility. This makes Cotton Linter 100% Premium Grade a preferred choice for customers who prioritize sustainability in their supply chain.As a trusted and established supplier in the cotton industry, (company name removed) has built a strong reputation for delivering high-quality products and exceptional customer service. The introduction of Cotton Linter 100% Premium Grade further strengthens the company's position as a go-to source for premium-grade cotton products, backed by reliable supply, competitive pricing, and a commitment to customer satisfaction.The launch of Cotton Linter 100% Premium Grade (brand name removed) reinforces (company name removed)'s dedication to innovation and meeting the evolving needs of its customers. By expanding its product range to include this premium-grade cotton linter, the company is well-positioned to cater to the growing demand from industries that require top-quality raw materials for their manufacturing processes.In conclusion, the introduction of Cotton Linter 100% Premium Grade by (company name removed) is a significant development that underscores the company's commitment to providing high-quality and sustainable cotton products to its customers. With its exceptional purity, reliability, and environmental considerations, this new offering is set to make a positive impact in various industries and further solidify (company name removed)'s position as a leading supplier of premium-grade cotton products.
Read More
Top A-Grade Nitrocellulose Solution Exporter from China
Certainly! Please provide the company introduction or any additional details you want included in the news article, and I will draft an 800-word news piece about the China A-Grade Nitrocellulose Solution exporter without mentioning the brand name.
Read More